During a factory quality audit for a skincare contract manufacturer, a brand should inspect six core areas — production environment, equipment and calibration, quality control systems, documentation and batch records, personnel and training, and material handling and storage. Certifications on paper confirm that a system existed on the audit day; an on-site walk-through confirms whether that system runs every day. This article breaks down what to check in each area and which red flags should prompt immediate follow-up.
Why Does an On-Site Audit Matter Beyond Certificates?
ISO 22716 and GMPC certificates tell you a factory passed an inspection — once. They do not tell you whether the same discipline holds on a random Tuesday when the auditor is not there. An on-site factory quality audit lets you observe real workflows, ask operators questions, and spot gaps that paperwork hides. For a brand entrusting its formula and reputation to a contract manufacturer, the visit is not a formality — it is risk management.
Think of it this way: the certificate proves the factory can meet a standard; the audit proves it does, consistently.
Production Environment — What Should You Look For?
Walk the production floor and filling room with these checkpoints in mind:
- Cleanroom classification: Filling operations for cosmetics typically require ISO 8 (Class 100,000) or better. Ask for the cleanroom validation report and check that air-change rates and HEPA filter status are documented.
- Pressure differential: Clean areas should maintain positive pressure relative to surrounding corridors. A visible pressure gauge or monitoring system confirms this.
- Temperature and humidity: Production areas need controlled conditions. Ask for recent monitoring logs — are they continuous (data logger) or manual? Gaps in records are a warning sign.
- Water system: Purified water (RO or DI) feeds most cosmetic formulations. Check that TOC, conductivity, and microbial counts are monitored regularly and that results stay within specification.
- Pest control and facility maintenance: Request pest-control service reports and facility maintenance logs. A well-run factory tracks these systematically.
Equipment and Calibration — What Must You Verify?
Equipment condition directly affects batch consistency. Check the following:
- Calibration stickers: Every measurement instrument — balances, pH meters, viscometers — must display a calibration sticker with a valid date. Expired or missing stickers indicate the factory does not enforce its own SOPs.
- Mixing and filling capacity: Confirm that tank sizes and filling-line speeds match your expected order volumes. Overloaded equipment leads to shortcuts.
- Cleaning validation: Ask how equipment is cleaned between products (CIP systems or manual procedures) and whether cleaning validation records exist — especially for shared equipment.
- Filling accuracy: Review weight-control samples and reject records from recent runs. High reject rates or no reject records both tell a story.
Quality Control Systems — Where Is the Real Proof?
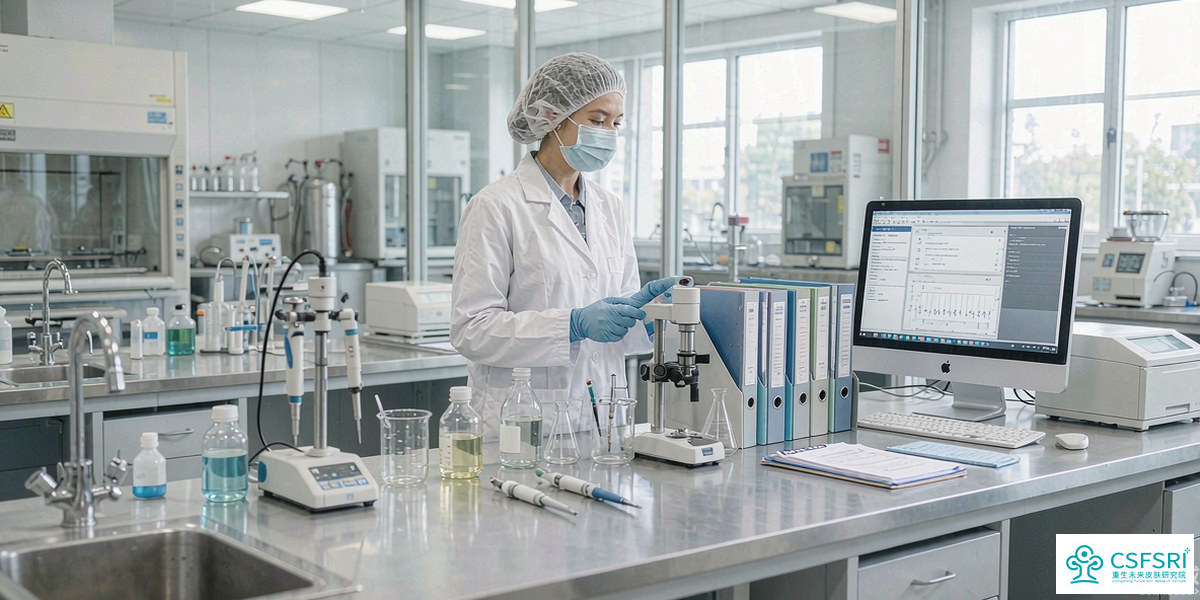
A robust QC system catches problems before they leave the factory. Evaluate these layers:
- Incoming raw material inspection: Does the factory verify every COA? Are identity tests (FTIR, HPLC) performed, or do they rely solely on supplier paperwork? Materials should move through a quarantine-then-release flow.
- In-process controls: Check that pH, viscosity, appearance, and temperature are recorded at defined steps during production — not filled in after the batch is complete.
- Finished product testing: Microbial limits, heavy metals, preservative efficacy, and stability testing should all be part of the release protocol. Ask which tests are run in-house versus sent to external labs.
- Retain samples: Confirm that retain samples are stored under controlled conditions, in sufficient quantity, and kept for an appropriate period — typically one to three years past the product expiry date.
- OOS and CAPA: When a result falls out of specification, is there a documented investigation and corrective action? The absence of OOS records often means problems are simply not recorded.
Documentation and Batch Records — How Do You Judge Integrity?
Batch records are the legal and operational backbone of GMP compliance. When reviewing them:
- Completeness: Every step should be recorded at the time it happens (contemporaneous). Pre-filled data, white-out, or blank signature fields are serious red flags.
- SOPs at workstations: Operators should have immediate access to the current version of relevant SOPs. Ask to see the SOP at the mixing station — is it the version the quality department approved?
- Change control: Any change to a formula, process, or piece of equipment should go through a formal change-control procedure with documented approval.
- Deviation records: Deviations happen in every factory. The question is whether they are documented, investigated, and resolved. A factory with zero deviation records is either exceptionally disciplined or not recording them.
- Recall readiness: Ask when the last mock recall was conducted. A documented mock recall tests whether the traceability system actually works under pressure.
Personnel, Training, and Hygiene — What Do You Observe?
People run the system, and their behavior reveals whether training has taken root:
- Training records: Every production and QC staff member should have a training file — job-specific skills plus GMP awareness. Check for recency and documented refresher courses.
- Gowning and hygiene: During your visit, watch whether workers follow gowning procedures: hair covers, masks, gloves, no jewelry, no food in production areas. If compliance slips while you are watching, it slips more when no one is.
- QC independence: The quality control team should be organizationally independent from production. If the QC manager reports to the production manager, conflict-of-interest risks increase.
- Staff turnover: High turnover disrupts knowledge continuity. While not always visible during a short visit, ask about it — factories with stable teams tend to maintain more consistent practices.
Material Handling and Storage — What Conditions Reveal Risk?
How a factory stores and moves materials shows whether its quality system extends beyond the lab:
- FIFO or FEFO: Raw materials and finished goods should follow first-in-first-out or first-expiry-first-out discipline. Ask how the system is enforced — software tracking, color-coded labels, or verbal instruction.
- Segregated storage: Approved, quarantined, and rejected materials must be physically separated. If a rejected drum sits next to an approved one without clear barriers, cross-use risk rises.
- Warehouse conditions: Temperature and humidity should be monitored in storage areas with alarm systems for excursions. Check recent excursion logs — were they investigated?
- Labeling integrity: Every container — raw material, work-in-progress, or finished product — should carry a clear status label. Unlabeled containers in any area are a compliance gap.
Which Red Flags Should Stop You in Your Tracks?
Some findings deserve immediate follow-up or a decision to walk away:
- Expired or missing calibration stickers on critical instruments
- Batch records with pre-filled data, white-out corrections, or unsigned steps
- No in-house QC lab — all testing outsourced with no internal verification capability
- Missing or improperly stored retain samples
- Workers ignoring gowning or hygiene rules during your visit
- No documentation of deviations, OOS investigations, or mock recalls
None of these alone means the factory is unsafe — but each signals that the quality system may have gaps wider than the certificates suggest. The purpose of a factory quality audit is to find these gaps before your product is on the line.
Planning your first factory visit or need a contract manufacturer that already meets the standard? CHONGSHENG FUTURE operates under ISO 22716 and GMPC compliance with transparent audit access — reach out to schedule a walk-through and see the process for yourself.